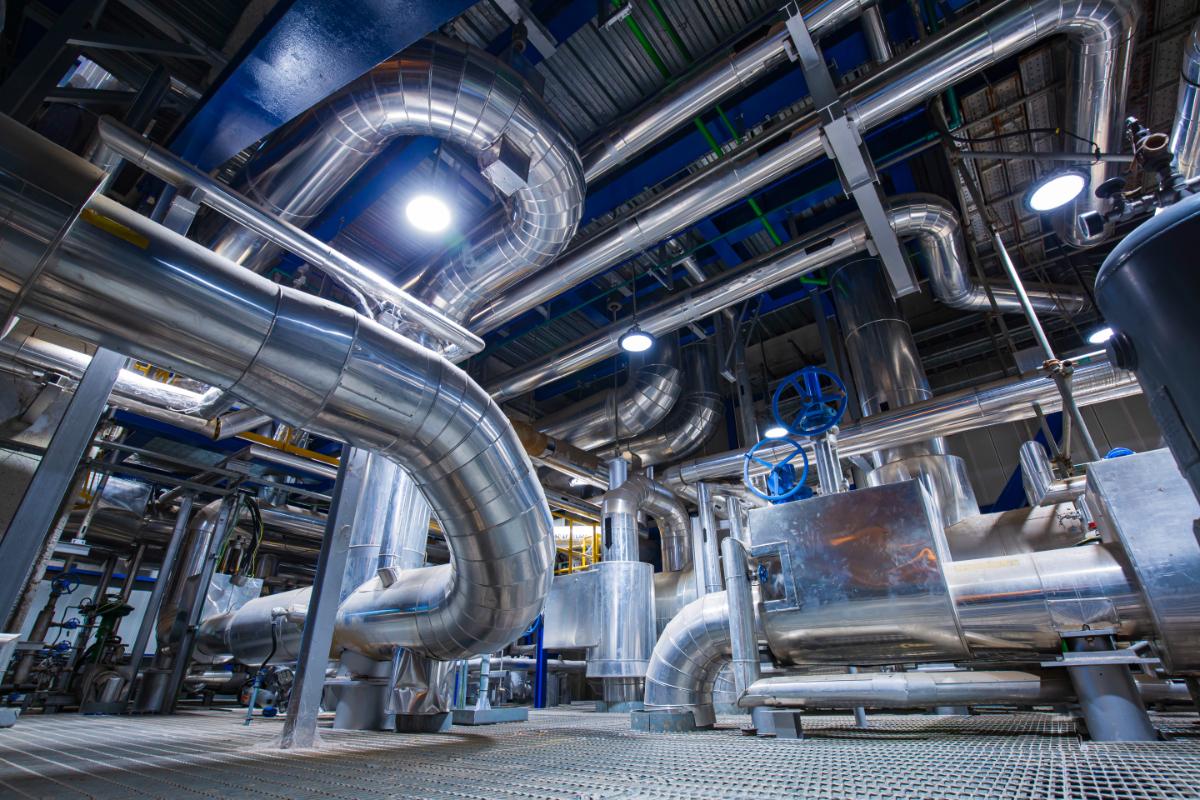
Coded welding for industrial pipework combines tested welding skills, controlled procedures and documented inspection. Its main benefits are greater consistency, clearer evidence of weld quality and a better basis for managing safety, reliability and maintenance costs. These advantages matter when pipes carry steam, gas, oil, water or hazardous chemicals through an industrial facility. Coded welding matters because the ability to produce a strong joint must be supported by evidence that it is suitable for its intended purpose.
Not all welding is subject to the same requirements, and not all qualifications are created equal. Coded welders must be qualified for the work they actually perform. In this blog, we explore how that distinction affects quality and safety, what customers should check and why a certificate alone cannot prove that a finished system is fit for use.
What Is the Difference Between Coded and Standard Welding?
The term standard welding is often used informally for general fabrication without a specified welder qualification requirement. It is not a recognised quality grade. Standard welding can still involve trained people, sound technique and careful inspection; the difference is whether a defined code-based qualification and acceptance framework is required for the project.
Coded welders have passed practical tests for a stated range of work. Their qualifications identify limits relating to the specific welding process, materials, joint types, thicknesses and positions. Certified welders who have passed one test are not automatically approved for every material or application. The key differences are the demonstrated scope of competence and the records supporting it, rather than a promise that coded work is always flawless.
When comparing coded welding with standard welding, ask what evidence the contract requires. Standard welding may be appropriate for some non critical applications, but pressure equipment and other critical applications can need formal certification and additional controls. Coded welders bring relevant qualifications to those projects, while the employer remains responsible for matching their skills to the task.
More Consistent Welds and Stronger Quality Control
Coded welding ensures that a defined qualification framework is applied when it is carried out correctly to the specified codes. Coded welders use a welding procedure specification, or WPS, that sets the permitted parameters for the joint. These can include preparation, consumables, heat input controls and other conditions outlined for the work. Following an appropriate WPS helps reduce variation between welders and between successive joints.
This consistency supports structural integrity, strength and durability. However, coded welding does not automatically make a joint defect free or corrosion resistant. Materials, design, operating conditions and workmanship all affect the final product. A weld may look smooth while containing internal defects, so ensuring that welds meet the required standards involves more than appearance.
Coded welders also need to understand when to stop and report a mismatch. If the available material, access or joint preparation differs from the approved instructions, improvising can compromise the result. Good quality assurance gives welders a clear route for resolving issues before they become costly repairs. This is especially important where components have been built to detailed specifications and small dimensional errors can lead to poor fit-up.
Reduced Safety Risks in High Pressure Pipework
Industrial environments can expose pipework to high pressures, extreme temperatures, vibration and corrosive fluids. In oil refineries, chemical plants and power stations, failure can create serious safety risks, including burns, toxic releases, fires or explosions. Coded welders help control these risks by working within suitable qualifications and procedures, supported by competent supervision.

For high pressure systems, the aim is to reduce the likelihood of leaks and structural failures. Coded welders must work to the specified acceptance criteria, with testing selected to suit the likely defects and service conditions. Ensuring safety also requires correct design, suitable supports and a safe installation; welding is a critical part of that wider system, not its only safeguard.
High pressures alone do not explain every hazard. Stored energy, fluid type and the consequences of failure are also important. Pressure vessels and associated pipes can contain substantial energy even when the equipment appears small. For safety critical applications, decisions must reflect these risks rather than the size or price of the welding job.
Better Control of Materials, Corrosion and Service Life
Choosing suitable materials is as important as choosing qualified welders. Stainless steel pipework, for example, still needs appropriate preparation, consumables and control of contamination. Coded welders working with specific materials must use welding processes and qualifications that cover those materials. An otherwise acceptable technique may be unsuitable for a different metal or service condition.
Long-term integrity also depends on environmental conditions. Pipework exposed to demanding conditions may need corrosion allowances, protective measures or planned monitoring. A durable system is built by considering these factors together. Welding alone cannot guarantee longevity under extreme conditions or prevent corrosion caused by an unsuitable material choice.
Maintaining records of material identity and joint locations helps future engineers understand what is installed. When repairs or modifications are required years later, this information can make it easier to select compatible components and suitable welding methods, supporting the useful life of the system.
Cost Savings Through Less Rework and Downtime
The commercial benefits of coded welding come from controlling preventable mistakes. Planning qualifications, access and inspection before fabrication starts can avoid rejected welds, repeated testing and delays during commissioning. For projects with a tight shutdown window, ensuring that the correct documentation is available can be just as valuable as completing the physical work quickly.
Coded welders can help a business manage costs by following a repeatable process and identifying problems early. Investing in competent people and appropriate testing may increase the initial budget, but can reduce rework and unplanned downtime in the long run. No fixed saving is guaranteed: the benefit depends on the installation, operating duty and quality of the overall project management.
Even small repairs deserve proper planning. Replacing a short pipe section on a safety critical line may require isolation, an approved repair method and examination before return to use. Ensuring that the scope is understood at the start helps critical projects stay on schedule without sacrificing safety and quality.
Welding Codes, Standards and Legal Requirements
Welding codes are technical rules for particular applications. Some codes address personnel qualifications, others qualify welding processes, and construction codes set requirements for the equipment itself. Understanding this distinction helps customers specify work accurately. Codes and standards should be identified by their actual designation and applicable edition, rather than a broad reference to the highest standards.

BS EN ISO 9606-1 addresses qualification testing of welders for fusion welding of steels. ASME IX addresses qualification of welding procedures and personnel. These are widely used, but their scopes and qualification rules differ. ASME codes for piping or pressure vessels may impose further construction requirements beyond Section IX. Ensuring that the correct combination is specified is crucial to compliant work.
The American Welding Society also publishes specific welding codes, including standards for structural steel and aerospace applications. Structural welding for load bearing structures, bridges or load bearing frameworks should not be confused with pressure vessel welding. A qualification for one type of structure does not automatically satisfy the welding requirements for another. Coded welders need qualifications that match the specific codes invoked by their projects.
Industry standards are not all legal requirements. Whether coded welding is mandatory depends on the equipment, relevant legislation and contract. UK safety regulations and industry regulations may require evidence that equipment is safe, while customer specifications can add further controls. International regulations must also be assessed for projects delivered overseas. Adherence to welding codes supports compliance, but does not by itself prove compliance with every legal obligation.
Current Standards Fact: Manual and Automated Welding Differ
As checked in September 2026, ISO lists ISO 9606-1:2012 as current, following confirmation in 2023, while a replacement remains under development. Its published scope covers manual and partly mechanised welding processes, not fully mechanised or automated welding processes. This is a useful distinction when comparing hand welding with automated production: different personnel qualification arrangements may be required.
For projects specifying BS EN ISO standards, confirm the applicable national adoption and edition with the responsible welding specialist. Certified welders should be able to show that their records match the process and positions in use. Ensuring that qualifications are current is more meaningful than assuming a certificate remains suitable simply because the holder passed a test in the past.
Choosing the Right Welding Process
Tungsten inert gas welding, usually called TIG welding, uses a non-consumable tungsten electrode and an inert gas shield. TIG can provide close control for pipe roots and thinner materials. Metal inert gas welding, or MIG welding, uses continuously fed wire and inert shielding gas; the related MAG process uses active shielding gas. MIG and MAG are often grouped together in conversation, but their technical distinction matters when selecting specific welding methods.
Manual metal arc welding, also known as MMA welding or stick welding, uses a flux-coated electrode. Different welding techniques offer different practical advantages, and no single process is best for every application. The right welding process depends on the metal, access, production needs and specified quality standards. Coded welders must follow the method accepted for the job rather than substitute a familiar technique without approval.
The success of pipe welding also depends on joint preparation and fit-up. Misalignment, poor cleanliness or unsuitable access can make achieving high quality welds more difficult. Precision during preparation is essential. Experienced welders and mechanical engineers should resolve these questions before work begins, ensuring that the proposed method can be carried out reliably on site.
Inspection and Testing: What Each Method Can Tell You
Visual checks can identify surface condition, alignment and visible imperfections, but cannot reveal every internal problem. Non destructive testing, commonly shortened to NDT, examines welds without deliberately breaking the component. Ultrasonic testing uses high-frequency sound to investigate the material, while dye penetrant testing helps reveal surface-breaking imperfections on suitable non-porous surfaces.
An important limitation is that penetrant testing cannot reveal a crack wholly beneath an intact surface. Ultrasonic examination also has limitations related to geometry, material and access. NDT methods must therefore be chosen for the expected damage or defect type. Not every weld requires the same examination, and the extent of testing must follow the applicable codes, inspection plan and contract.
Destructive testing is different: specimens are cut, bent, pulled or otherwise tested in ways that damage or consume them. Destructive testing may be used to qualify a welding procedure or a welder, according to the relevant rules. Production joints are then inspected using the agreed acceptance process; a qualification test does not replace examination of the finished work.
Coded welders should work with the inspector to ensure that welds meet the specified acceptance criteria. Records should document what was examined, by whom and with what result. This evidence helps verify weld quality and identify cracks, porosity or other imperfections requiring assessment. Testing supports quality and safety; it does not provide unlimited guarantees about future performance.
Pressure-System Safety: A Welding Certificate Is Not an Examination Scheme
HSE states that qualifying pressure equipment needs a written scheme of examination and an examination before use. This is separate from the records held by coded welders. A qualification certificate cannot replace the duties of the owner or user under the Pressure Systems Safety Regulations 2000, including maintaining the appropriate examination arrangements.
Pressure-system scope has details that are easy to miss. HSE identifies steam at any pressure and, subject to the regulations and exceptions, compressed or liquefied gas above 0.5 bar gauge as relevant fluids. Systems do not have to operate at extreme pressures to warrant attention. Conversely, not every system operating at high pressures falls under the same rules. A competent person should establish what applies to the actual equipment.
Maintaining compliance therefore extends beyond construction. Users need suitable examination and maintenance arrangements for pressure vessels, protective devices and associated pipework. This distinction matters when planning new projects or bringing modified equipment back into service. It helps ensure safety remains part of the operating plan after the welders have completed their work.
Traceability and the Documents Customers Should Receive
Coded welding ensures that personnel qualification is addressed within the specified framework; customers also need evidence of how the work was controlled. Depending on the contract, the handover package may include welder qualification records, procedure references, material certificates, weld maps and inspection or testing reports. These documents connect individual joints to the people, materials and acceptance checks involved.
Ask which records are included before appointing a contractor. Certified professionals should explain what their formal certification covers and what further approvals the project needs. Codes define different acceptance routes, so a company should not offer the same document pack for all projects without reviewing the requirements. Ensuring that records are complete makes future inspections, modifications and audits easier.
In manufacturing and other industries with high demand for traceability, missing records can delay acceptance even when the physical work appears satisfactory. Coded welders and supervisors should agree how records will be collected during production. Building documentation into the process is generally more reliable than reconstructing it afterwards.
Agreeing Project Checks Before Work Starts
An inspection and test plan can be developed to show when checks are required and who must perform them. For example, an agreed hold point may prevent work continuing until a joint preparation or test result has been accepted. Its role is to make responsibilities clear, giving trained personnel enough time to meet the specified safety standards without making decisions under production pressure.
For UK projects, the client and contractor should identify applicable regulatory requirements alongside industry standards. Adhering to a plan helps maintain compliance, but the plan itself must address the correct obligations. If a tender refers only to regulatory standards, ask which rules it means. Specific acceptance criteria help teams meet expectations and comply with the contract. Safety is paramount, and a clear agreement about the required level of examination is essential to putting that principle into practice.
Where These Benefits Matter Most
Many industries require coded welding where the consequences of a failed joint justify controlled qualifications and inspection. Oil and gas, chemical processing, energy, food manufacturing and water treatment are familiar examples. Aerospace and other specialist sectors can impose additional customer approvals. Coded welders serving these industries must work within the scope required for the equipment, rather than relying on general experience alone.
Across industries, the key question is how the pipework will be used. High pressures, corrosive fluids, temperature cycling and restricted maintenance access can all influence the required standards. In industries handling hazardous materials, strict standards support efforts to meet safety and quality standards and reduce the chance of catastrophic failure. The selected controls should reflect the service conditions and consequences, not merely a claim to the highest standards.
The importance of traceability often becomes clearest during a later modification. Without reliable records, an engineer may need additional investigation to establish the materials and original acceptance basis. Pipelines and plant pipework should be assessed against their own duties; experience from a similar project cannot replace a review of current requirements.
Conclusion: Choosing Coded Welding Services
Choosing a provider starts with the actual duty of your pipes and equipment. Share drawings, operating conditions, material details and the codes specified for the work. Ask how the team will meet code requirements, confirm qualifications and manage inspection. The best answer explains how safety and quality will be controlled and what evidence will be available when the work is finished.
At Anderson Engineering And Welding Services, we provide coded welding services and engineering expertise for industrial pipework. Contact our team today to discuss the scope, available documentation and any specific codes your projects must meet. We can help you find practical next steps for fabrication, installation or repair, based on the requirements of your system.